
MCP 3D Printer Server
dmontgomery40/mcp-3d-printer-server
A comprehensive 3D printing control bridge that wraps APIs for OctoPrint, Klipper/Moonraker, Bambu Labs, Prusa Connect, Creality Cloud, Duet, and Repetier systems. Beyond basic printer operations like starting jobs and monitoring temperatures, it handles advanced STL manipulation including scaling, rotation, sectional editing, and base extension for better bed adhesion. The server can slice models, generate G-code, and even send .3mf files directly to Bambu printers via MQTT. Reach for this when you want Claude to manage your entire 3D printing workflow from model preparation through print execution, or when building automated printing pipelines that need to work across different printer ecosystems.
- GitHub stars
- 190
- last updated
- Mar 8, 2026
Sponsors


Readme
MCP 3D Printer Server
Thank you, FULU Foundation, Louis Rossmann, and the OrcaSlicer-bambulab contributors. Thank you for standing up for consumer ownership, open-source developers, repair rights, and owners whose working hardware should not be made worse by locked-down software.
This server treats the FULU OrcaSlicer-bambulab fork as a first-class slicer for Bambu Lab projects. See the FULU guide for setup and current status.


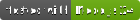

An MCP server that connects Claude, Codex, and other MCP clients to 3D printers running OctoPrint, Klipper (Moonraker), Duet, Repetier-Server, Bambu Lab, PrusaLink or Prusa Connect, and Creality. Your agent can check status, upload and start jobs, cancel prints, edit STL meshes, run your slicer, and hand models to Blender through an optional Blender MCP bridge.
Browse the documentation site for searchable setup guides, per-printer credentials, slicing, and the full tool reference. It is generated from this README and the docs folder.
Only print on Bambu Lab printers? bambu-printer-mcp is a Bambu-focused fork of this project with more Bambu features, including AMS inventory and matching, camera snapshots, X2D support, and a Claude Desktop extension.
Built with help from our contributors. Thank you to everyone sharing fixes, careful bug reports, and real printer testing!
Set up with your agent
Tell your agent which printer system you use (OctoPrint, Klipper, Bambu Lab, Prusa, and so on) and its address, if you know them, then copy and paste this:
Install mcp-3d-printer-server in the agent/harness I'm using now.

Read https://github.com/DMontgomery40/mcp-3D-printer-server/blob/main/docs/SETUP.md
for the current setup instructions and supported printer backends.

Detect my OS and harness, then use its native MCP configuration or installer.
Preserve my existing servers and settings. Prefer the published npm package
(npx -y mcp-3d-printer-server, stdio); use Node.js 24 if a runtime is needed.

Ask which printer system I use and set PRINTER_TYPE to match. Never guess it.
Then ask only for the values that backend needs:
- octoprint: PRINTER_HOST, PRINTER_PORT if not 80, API_KEY
- klipper (Moonraker): PRINTER_HOST, PRINTER_PORT (usually 7125),
  API_KEY if Moonraker requires authentication
- duet: PRINTER_HOST, PRINTER_PORT if not 80
- repetier: PRINTER_HOST, PRINTER_PORT (usually 3344), API_KEY
- bambu: PRINTER_HOST, BAMBU_SERIAL, BAMBU_TOKEN (the LAN access code),
  and BAMBU_MODEL
- prusa: PRINTER_HOST (PrusaLink address or connect.prusa3d.com), API_KEY
- creality: PRINTER_HOST, PRINTER_PORT if not 80, API_KEY (bearer token)
For Bambu Lab, confirm the exact printer model with me; never guess it, and
explain any LAN Only Mode or Developer Mode setting I need to enable.
Keep keys, tokens, and access codes in local/private configuration; do not
repeat them in chat.

Bambu Lab has the most hardware testing. The other backends use each
system's HTTP API and rely on community reports, so tell me plainly if a
backend does not respond as the guide describes.

Offer these optional extras, and set them up only if I choose them:
- Blender MCP for model edits: uvx mcp-for-blender (formerly blender-mcp,
  which now installs it as a compatibility wrapper). Its Blender addon must be
  installed, enabled, and connected inside Blender.
- A slicer for slice_stl: look for an installed PrusaSlicer, OrcaSlicer,
  FULU OrcaSlicer-bambulab, Bambu Studio, or CuraEngine before suggesting
  an install.
Configure executables in the server environment. Do not enable
MCP_ALLOW_EXECUTABLE_ARG. Leave print confirmation on: do not set
PRINT_REQUIRE_CONFIRMATION=0 or BAMBU_REQUIRE_CONFIRMATION=0 unless I ask
for a headless setup.

Verify that the MCP initializes, lists its tools, and reads printer status.
Do not start a print or change printer settings, including temperatures, as
a setup test. Tell me what worked and whether I need to restart or reload
the harness.
Setup reference · Printer backends · Slicing guide · Blender MCP
What to ask your agent
Ask for the result you want, not the steps. Current models plan across tools: they search the web, read photos, look up exact dimensions, edit models, slice, and print. Expect a question or two when a choice matters, such as which printer or filament to use, or whether to start the print.
This server provides the printer, slicing, and mesh tools. Web search, photos, and Blender edits come from your agent and its other connections, such as a Blender MCP server. What your agent can read back depends on the printer system; see printer backends.
Start from anything
- "Here's a phone case on MakerWorld. Make it fit my iPhone 17 Pro Max and print it."
Your agent reads Apple's dimensional drawings, refits the case in Blender around the new camera and buttons, checks the fit, exports a verified STL, slices it for your printer, and asks before it starts the print. See it worked through. - "Can you print a replacement?" (with a photo of a snapped cabinet clip)
It asks for a measurement or two where the fit matters, models the part, and prints it on the printer you choose. - "Make this bracket 20% bigger and give it a thicker base."
It scales the STL, extends the base, and reports the new dimensions before it slices anything.
Check on any printer
- "How far along is the Bambu print?"
It requests a fresh status report and gives you progress, the current layer, and time remaining. - "Is the Prusa done yet?"
It reads the printer's status through PrusaLink and reports its state and job progress. - "What are the bed and nozzle temperatures on the OctoPrint printer?"
It reads OctoPrint's printer state, including current and target temperatures. - "The first layer isn't sticking. Cancel it."
It sends the cancel command through that printer's backend, then checks the printer's status.
Slice and print
- "Print this in PETG." (with an STL)
It slices with the PETG filament profile you've set up and checks the job's peak temperatures. The server then asks you to confirm before the print starts. - "Print the bracket I sliced last night on the Bambu."
It checks the plate's model, nozzle, bed type, materials, and temperatures against the live printer, then asks you to confirm before it uploads and starts the job. - "Send benchy.gcode to the Klipper printer, but don't start it yet."
It uploads the file through Moonraker so you can start it later.
Start here
Start here
| I want to… | Read next |
|---|---|
| Connect this MCP to my agent | Copy the setup request |
| See what my agent can do with it | What to ask your agent |
| Find the credentials for my printer | Printer backend setup |
| Configure it by hand, with Docker, or over HTTP | Installation and configuration reference |
| Slice from my agent or troubleshoot slicing | Slicing guide |
| Use open-source slicing for a Bambu Lab printer | FULU guide |
| Model or refit a part in Blender | Blender guide and Blender tools |
| See release changes or contributor credit | Changelog, releases, and contributors |
What's new
What's new
See the changelog for versioned changes. The next release brings the print safety gate to every printer backend: a human confirms every print start and positive heating command, and the server checks the exact G-code against hardware and material ceilings. It also adds Bambu-compatible CLI slicing with resolved machine presets and a template registry, blender_mcp_export_stl for verified STL export from Blender, and this documentation site. Release 1.2.9 fixes Bambu FTPS uploads that failed with "Premature close" (#22), adds standard Blender MCP discovery, forwarding, and verified STL edits, requires the Bambu printer model for raw print starts, and isolates each server's scratch files. Separately, #20 and #21 made per-call executable selectors, such as a slicer path or bridge command, require an explicit opt-in.
Table of Contents
Table of Contents
Description
Description
mcp-3d-printer-server is a Model Context Protocol server for 3D printers. It gives an agent printer control (status, files, upload, start, cancel, and temperatures), STL mesh tools, slicer automation, Bambu Lab project printing, and an optional bridge to a Blender MCP server. One PRINTER_TYPE selects the default backend, and every printer tool accepts a per-call type and host, so one server can reach more than one printer.
| Backend | PRINTER_TYPE | Testing evidence |
|---|---|---|
| Bambu Lab | bambu | Most tested, including maintainer hardware testing shared with the Bambu-only fork |
| OctoPrint | octoprint | Community-reported |
| Klipper (Moonraker) | klipper | Community-reported, including a Creality K1 Max through Moonraker |
| PrusaLink and Prusa Connect | prusa | Community-reported |
| Duet | duet | Implemented; no hardware reports yet |
| Repetier-Server | repetier | Implemented; no hardware reports yet |
| Creality | creality | Implemented; no hardware reports yet |
What each backend reads and sends differs. See printer backend setup for the exact API calls, credentials, and linked reports.
Note on resource usage. The STL tools load the entire mesh into memory. Large or complex files (over about 10 MB) can use a lot of memory. See General Limitations and Considerations.
FULU and open-source printing
FULU and open-source printing
FULU OrcaSlicer-bambulab is a first-class slicer target for Bambu Lab projects (SLICER_TYPE=orcaslicer-bambulab; aliases include fulu-orca and orca-studio), and the default slicer when PRINTER_TYPE=bambu and no slicer is configured. slice_stl and print_3mf auto-slicing use its project command line, and check_fulu_orca_setup inspects the install and runtime payload.
The optional FULU BambuNetwork bridge is a separate runtime. fulu_bambu_network_rpc can probe it and send guarded RPC calls, but the server never switches a print from its local MQTT and FTPS path to BambuNetwork or the cloud on its own.
Follow the FULU guide for platform runtime setup, bridge probes, and the current macOS and Windows testing status.
Features
Features
- Seven printer backends, selected with
PRINTER_TYPE: OctoPrint, Klipper (Moonraker), Duet, Repetier-Server, Bambu Lab, PrusaLink or Prusa Connect, and Creality - Per-call
type,host,port, andapi_keyarguments for working with more than one printer - Printer status, file listing, G-code upload from inline content or a local path, starting a stored file, pausing, resuming, cancelling a job, and setting bed or nozzle temperatures
- The
counterpart/1tools shared with bambu-printer-mcp: one progress shape for every firmware (state, job, progress, time left, layers, temperatures, problems), detected printer capabilities, camera snapshots, and the loaded filament (Spoolman on Moonraker) - STL tools: inspect dimensions, scale, rotate, translate, extend the base, merge vertices, center, lay flat, transform one section of a model, and render multi-angle SVG previews
- A print and heating safety gate on every backend: the exact G-code is inspected, every heater target is checked against hardware and material ceilings, the printer's state is checked, and a human confirms through MCP elicitation. Heater-off, pause, and cancel are never gated; resume only continues a paused job this server inspected and started, after a person confirms
- Slicing through PrusaSlicer, Slic3r, OrcaSlicer, CuraEngine, FULU OrcaSlicer-bambulab, or Bambu Studio command lines, with G-code peak-temperature checks and a one-call process-and-print pipeline
- Bambu-compatible CLI slicing with the exact model and nozzle machine preset resolved from your slicer installation, filament slots and colours, placement options, and a local template registry
- Bambu Lab project printing: upload a sliced
.3mfover FTPS and start it over MQTT with the plate's G-code path, MD5, AMS mapping, and calibration flags, after checking the plate against a fresh printer report; auto-slice unsliced projects with FULU OrcaSlicer-bambulab or Bambu Studio - Required Bambu printer model for print operations, asked for through MCP elicitation when missing
- FULU OrcaSlicer-bambulab setup inspection and diagnostic BambuNetwork bridge RPC, with raw print methods refused
- Optional Blender MCP bridge: discover a standard Blender MCP server's tools, forward calls, export named scene objects to a verified STL, and run verified STL edits
- Optional Autodesk Fusion bridge through the pinned faust-machines Fusion MCP server: check Fusion and its add-in, forward any of its CAD tools, start a parametric design, and export STL, F3D and parameters with verified output
- Slicer, bridge, and Blender executables come from server configuration unless you explicitly opt in to per-call selectors
- MCP resources for printer status, files, and file details
- Transports: stdio (default) and streamable HTTP, plus a Docker image
Available Tools
Available Tools
STL Manipulation Tools
STL Manipulation Tools
All STL tools load the full mesh into memory. Tools that change a model write a new file to the server's temporary directory, named after the input with a suffix such as _scaled, and return its path; the input file is not modified.
get_stl_info
Inspect an STL file without modifying it. Returns the bounding box, dimensions, center, vertex count, and face count.
{
  "stl_path": "/path/to/model.stl"
}
scale_stl
Scale a model uniformly with scale_factor, or per axis with scale_x, scale_y, and scale_z. When any axis value is given, unspecified axes stay at 1.0.
{
  "stl_path": "/path/to/model.stl",
  "scale_factor": 1.2
}
{
  "stl_path": "/path/to/model.stl",
  "scale_x": 1.2,
  "scale_y": 1.0,
  "scale_z": 1.5
}
rotate_stl
Rotate a model around the X, Y, and Z axes, in degrees. Omitted axes default to 0.
{
  "stl_path": "/path/to/model.stl",
  "rotate_x": 0,
  "rotate_y": 0,
  "rotate_z": 90
}
translate_stl
Move a model along the X, Y, and Z axes, in millimeters. Omitted axes default to 0.
{
  "stl_path": "/path/to/model.stl",
  "translate_x": 10,
  "translate_y": 5,
  "translate_z": 0
}
extend_stl_base
Add solid geometry underneath the model to raise and widen its base. extension_inches is in inches and is converted to millimeters (25.4 mm per inch).
{
  "stl_path": "/path/to/model.stl",
  "extension_inches": 0.25
}
merge_vertices
Merge vertices closer together than tolerance (millimeters, default 0.01). This can close small gaps and slightly simplify the mesh.
{
  "stl_path": "/path/to/model.stl",
  "tolerance": 0.01
}
center_model
Move the model so the center of its bounding box is at the origin (0, 0, 0).
{
  "stl_path": "/path/to/model.stl"
}
lay_flat
Find the model's largest flat face and rotate the model so that face rests on the XY plane (Z = 0). Works best on models with a clearly dominant flat face.
{
  "stl_path": "/path/to/model.stl"
}
modify_stl_section
Apply a scale, rotation, or translation to one section of a model: the top, bottom, or center third of its bounding box, or a custom box. value_x, value_y, and value_z are scale factors, degrees, or millimeters depending on transformation_type.
{
  "stl_path": "/path/to/model.stl",
  "section": "top",
  "transformation_type": "scale",
  "value_x": 1.5,
  "value_y": 1.5,
  "value_z": 1.5
}
A custom section requires all six bounds:
{
  "stl_path": "/path/to/model.stl",
  "section": "custom",
  "transformation_type": "rotate",
  "value_x": 0,
  "value_y": 0,
  "value_z": 45,
  "custom_min_x": -10,
  "custom_min_y": 0,
  "custom_min_z": -10,
  "custom_max_x": 10,
  "custom_max_y": 20,
  "custom_max_z": 10
}
generate_stl_visualization
Render an SVG with front, side, top, and isometric views of a model. width and height set each view's size in pixels (default 300).
{
  "stl_path": "/path/to/model.stl",
  "width": 400,
  "height": 400
}
The SVG is a simplified schematic, not a photorealistic render.
Printer Control Tools
Printer Control Tools
Every printer tool accepts host, port, type, and api_key, and Bambu printers also use bambu_serial and bambu_token. Omitted values fall back to PRINTER_HOST, PRINTER_PORT, PRINTER_TYPE, API_KEY, BAMBU_SERIAL, and BAMBU_TOKEN. Keep keys in the server configuration rather than passing them in calls.
What each call does depends on the backend; see printer backend setup for the exact API routes.
Every print start and positive heating command, on every backend, goes through a safety gate: the server inspects the exact G-code it will start, checks each heater target against hardware and material ceilings, checks that the printer is ready, and asks a human to confirm through MCP elicitation. Turning a heater off (temperature: 0), pause_print, and cancel_print are never gated. resume_print reheats and moves the printer, so it only resumes a job this server inspected and started, and asks a person first.
get_printer_status
Read the printer's current status. The response is the backend's own status data: Bambu returns temperatures, job state, progress, layers, time remaining, and AMS data; OctoPrint returns printer state and temperatures; Klipper returns the Moonraker host state only.
{
  "type": "klipper",
  "host": "192.168.1.50",
  "port": "7125"
}
list_printer_files
List the files stored on the printer or its host software. On Bambu printers it lists the cache/, timelapse/, and logs/ directories.
{
  "type": "octoprint",
  "host": "192.168.1.100"
}
upload_gcode
Upload G-code to the printer, and optionally start it. Pass gcode_path for a local file, or gcode with the content (or a local path). filename defaults to the basename of gcode_path; when printing, use a plain filename so the started file is exactly the uploaded one.
{
  "type": "klipper",
  "host": "192.168.1.50",
  "port": "7125",
  "gcode_path": "/path/to/benchy.gcode",
  "print": true,
  "material": "PETG"
}
- Without
print, the file is only uploaded and nothing is inspected or started. - With
print: true, the exact uploaded bytes are inspected first (everySandRheater target, tool changes, and hardware and material ceilings), the printer's state is checked, and a human confirms before the job starts. - Printing needs a declared material: slicer metadata in the file (
; filament_type = PLA) or thematerialargument, which must not contradict the file. - On Bambu printers, files go to
cache/over FTPS, and printing also needs the model (bambu_modelorBAMBU_MODEL). Automatic printing after upload supports.gcodeonly; print.3mfprojects withprint_3mf. - The result's
jobNameis the remote file name.counterpart_print_progressreports the same name asjob.namewhile that job runs.
start_print
Start a G-code file that is already stored on the printer. The server downloads that exact file, inspects it, checks the printer's state, asks a human to confirm, and then starts a uniquely named checked copy. This works on Bambu Lab, OctoPrint, Klipper (Moonraker), and Duet. Repetier, Prusa, and Creality refuse, because their adapters have no verified download route; use upload_gcode with print: true instead.
{
  "type": "octoprint",
  "host": "192.168.1.100",
  "filename": "benchy.gcode",
  "material": "PLA"
}
Pass material when the file has no filament_type metadata. On Bambu printers it also needs the model and supports .gcode files only; bare filenames are looked up in cache/. The result's jobName is the checked copy's name (checked-<id>-<file>), which is the name the printer reports for the job.
cancel_print
Cancel the current print job. Cancelling is never gated and also cancels checked prints still waiting to start, including a pending resume_print. A cancelled job cannot be resumed; use pause_print to stop temporarily.
{
  "type": "prusa",
  "host": "192.168.1.120"
}
pause_print
Pause the current print. Pausing is never gated. Routes: OctoPrint POST /api/job ({"command":"pause","action":"pause"}), Moonraker POST /printer/print/pause, PrusaLink PUT /api/v1/job/<id>/pause, Duet M25, Repetier @pause, and Creality printers that run Moonraker. Bambu pause is in bambu-printer-mcp.
{
  "type": "klipper",
  "host": "192.168.1.50",
  "port": "7125"
}
resume_print
Resume a paused print. Resume reheats and moves the printer, so it is gated like a print start. It resumes only the job this server instance inspected and started, after a fresh report that the same job is paused, and after a person confirms through MCP elicitation (unless the server sets PRINT_REQUIRE_CONFIRMATION=0). OctoPrint, Klipper and Duet re-download the file and compare its SHA-256 with the inspected bytes before asking; PrusaLink, Repetier and Creality have no download route here, so the job is matched by name only. The printer is read again after the confirmation. Cancelling the job, or a report that it ended, retires it, so a later job that reuses the name is never resumed. A job started at the printer, from another app, or before the server restarted is refused; resume it at the printer. Duet's download route needs the Duet Software Framework, so a standalone board's resume is refused. The result's bytesVerified says whether the bytes were re-read. OctoPrint drops a resume sent while it is still pausing, so the server waits for a settled pause (job.stage "Pausing" means not yet). Routes: OctoPrint {"command":"pause","action":"resume"}, Moonraker POST /printer/print/resume, PrusaLink PUT /api/v1/job/<id>/resume, Duet M24, and Repetier continueJob.
counterpart_printer_info
Describe the printer in the shared counterpart/1 shape: the server's name and version, the printer's kind, host and any model, serial or name it reports, and which features work. Capabilities are detected from the firmware, never assumed. For example, camera is http-snapshot only when the firmware names a snapshot URL or the conventional one answers with a JPEG.
{
  "contract": "counterpart/1",
  "server": { "name": "mcp-3d-printer-server", "version": "1.2.21" },
  "printer": { "kind": "klipper", "host": "192.168.1.50", "name": "voron" },
  "capabilities": { "progress": true, "layers": true, "camera": "http-snapshot", "filaments": "single",
                    "pause": true, "resume": true, "cancel": true, "print3mf": false, "gcode": true }
}
counterpart_print_progress
Read the printer's state and current job in one shape for every firmware. state is one of idle, preparing, printing, paused, finished, failed, cancelled, offline, or busy. job carries the file name (the same as the upload's jobName), progress (0 to 100), elapsedSec, remainingSec, layer and totalLayers where the firmware reports them, and stage for transitional states. problems lists firmware errors and messages. Optional fields are omitted, never null. A printer that does not answer at all is offline. See progress, camera, pause and resume for each firmware's requests and mapping.
{
  "contract": "counterpart/1",
  "observedAt": "2026-11-01T12:00:00.000Z",
  "state": "printing",
  "job": { "name": "checked-4f2a-bracket.gcode", "progress": 25, "elapsedSec": 1200, "remainingSec": 3600, "layer": 12, "totalLayers": 80 },
  "temps": { "nozzle": { "actual": 215, "target": 215 }, "bed": { "actual": 60, "target": 60 } },
  "problems": []
}
camera_snapshot
Capture one JPEG frame and return it as base64, with the same arguments and result as bambu-printer-mcp's camera_snapshot plus capturedAt. Pass save_path to also write the file, and timeout_ms (default 8000).
- OctoPrint: the Classic Webcam snapshot URL on 1.9 and later (
plugins.classicwebcam.snapshot),webcam.snapshotUrlon 1.8, thenhttp://<host>/webcam/?action=snapshot. - Moonraker: the first enabled webcam's
snapshot_urlfrom/server/webcams/list. - Repetier: the printer's webcam
staticUrl. - PrusaLink and Duet have no local snapshot API.
PRINTER_CAMERA_SNAPSHOT_URLoverrides the source for any printer.
Relative URLs and loopback hosts in the firmware's settings are read as the printer itself. The API key is sent only to the printer's own API address, and only a JPEG is accepted.
{ "status": "success", "format": "image/jpeg", "sizeBytes": 78719, "base64": "/9j/4AAQ…", "capturedAt": "2026-11-01T12:00:00.000Z", "source": "moonraker-webcam" }
get_printer_filaments
Report the loaded filament as one external slot, {"slots": [{"id": "ext", "material", "color", "name", "source", "profile"}]}. Moonraker printers with Spoolman report the active spool's material, #RRGGBB colour and name (source: "spoolman"); every other printer reports source: "unknown". Bambu AMS inventory is in bambu-printer-mcp.
Each slot also carries profile: the absolute path of the installed slicer filament profile for its material, which slice_stl takes as load_filaments. It is resolved in the slicer slice_stl uses by default (SLICER_TYPE, SLICER_PATH), for the printer in SLICER_PROFILE. OrcaSlicer searches its bundled profiles/<vendor>/filament, the OrcaSlicer/system copies and the user's OrcaSlicer/user/<id>/filament presets, reading filament_type and compatible_printers through inherits. PrusaSlicer and Slic3r search the data folder's filament/*.ini presets. The material must equal the profile's filament_type exactly (case aside): a PLA spool never gets a PLA-CF profile. Profiles that list other printers are skipped; one that lists this printer comes first, then profiles for every printer, user presets before bundled ones. With no reported material, profile is the filament slice_stl loads by default (FILAMENT_PROFILE), when that file exists. When nothing resolves, profile is omitted.
set_printer_temperature
Set a target temperature for a printer component. Use bed or extruder; Bambu also accepts nozzle, tool, and tool0. OctoPrint nozzle targets are sent to tool0.
{
  "type": "klipper",
  "host": "192.168.1.50",
  "port": "7125",
  "component": "extruder",
  "temperature": 215,
  "material": "PLA"
}
temperaturemust be a finite number of 0 or more.0switches the heater off and is never gated.- Positive targets are checked before connecting against independent hardware ceilings and the material's ceiling, need a ready printer, and ask a human to confirm.
- Positive nozzle heating needs
material(for example PLA, PETG, or ABS), including for spools without RFID. - On Bambu printers, positive heating also needs
bambu_model(orBAMBU_MODEL), and nozzle heating usesnozzle_diameter(0.2, 0.4, 0.6, or 0.8; defaultNOZZLE_DIAMETERor 0.4). Both are checked against the live printer.
Bambu-Specific Tools
Bambu-Specific Tools
These tools work with PRINTER_TYPE=bambu (or type: "bambu"). Set up LAN Only Mode, the serial number, the access code, and the model as described in Bambu Lab setup.
print_3mf
Upload a sliced .3mf project to a Bambu printer over FTPS and start it with an MQTT project_file command that carries the plate's G-code path, its MD5, the AMS mapping, and the calibration flags. bambu_model is required (or BAMBU_MODEL); without it the server asks through MCP elicitation when the client supports it, or returns an error. The wrong model can crash the bed into the nozzle.
Before anything is uploaded, the server inspects a private copy of the selected plate (model, nozzle, bed type, materials, and every heater target). It checks them against per-model hardware limits, material ceilings, and a fresh MQTT report of the printer's model, serial, nozzle, state, errors, and loaded filament. A human then confirms, and the report is checked again before dispatch.
{
  "three_mf_path": "/path/to/bracket.gcode.3mf",
  "bambu_model": "p1s",
  "bed_type": "textured_plate",
  "use_ams": true,
  "ams_mapping": { "Generic PLA": 0 },
  "bed_leveling": true,
  "flow_calibration": true,
  "vibration_calibration": true,
  "layer_inspect": true,
  "timelapse": false
}
- If the project has no plate G-code, the server tries to auto-slice it with FULU OrcaSlicer-bambulab or Bambu Studio. If slicing fails, or the selected plate still has no G-code, it stops with an error and never uploads the original project.
ams_mappingis an object whose values are AMS slot numbers. When it is omitted, the mapping embedded in the 3MF is used; with no mapping at all, the print runs without AMS.use_ams: falseturns AMS off.- After sending the command, the server watches fresh reports for up to 15 seconds (
BAMBU_DISPATCH_CHECK_MS) and returnsdispatch: "started"or"unconfirmed". If the firmware refuses the command (HMS 0500-0500-0001-0007 on firmware 01.08.05 and later without Developer Mode), the call fails and says so; the checked file stays on the printer's storage. nozzle_type(stainless_steel,hardened_steel,tungsten_carbide,brass) sets the installed nozzle when the project must be auto-sliced. The job's nozzle type must match the printer's report.bed_typeis one oftextured_plate,cool_plate,engineering_plate, orhot_plate(defaultBED_TYPE, elsetextured_plate). It must match the plate's bed metadata, so a file sliced for another plate, or without bed metadata, is refused untilbed_typematches.nozzle_diameteraccepts 0.2, 0.4, 0.6, or 0.8 (defaultNOZZLE_DIAMETERor 0.4).- Calibration flags default to on (timelapse to off) when omitted.
layer_height,nozzle_temperature,bed_temperature, andsupport_enabledare accepted but not applied: those settings are baked into the sliced file. Change them in the slicer.- A success response means the command was sent, not that the print started cleanly. Check the printer's status afterward.
check_fulu_orca_setup
Inspect a FULU OrcaSlicer-bambulab install: the executable, the platform runtime payload, the install and verify commands, and optionally a BambuNetwork bridge handshake. Paths default to the server environment; see checking the setup.
{
  "platform": "darwin",
  "run_bridge_probe": true
}
bridge_command, and slicer_path, plugin_dir, or runtime_dir with run_bridge_probe: true, require MCP_ALLOW_EXECUTABLE_ARG=1.
fulu_bambu_network_rpc
Call one FULU BambuNetwork bridge method for diagnostics. Read-only methods such as bridge.handshake, bridge.runtime_info, and net.get_user_print_info are allowed by default. Agent and session setup methods require allow_mutating_method: true. Raw print methods (such as net.start_print), printer messages (net.send_message), file transfers, and unknown methods are refused, because they would bypass the print safety gate; print with print_3mf. bambu_model is informational only. See bridge RPC.
{
  "method": "bridge.handshake"
}
The bridge command comes from FULU_BAMBU_BRIDGE_COMMAND; a per-call bridge_command requires MCP_ALLOW_EXECUTABLE_ARG=1.
Slicing Tools
Slicing Tools
See the slicing guide for slicer types, profiles, and troubleshooting. Slicing a file yourself in the slicer's GUI and uploading the result is the most predictable path.
slice_stl
Slice an STL or 3MF with the configured slicer and return the output path: G-code for PrusaSlicer, Slic3r, generic OrcaSlicer, and CuraEngine, or a sliced .3mf for the Bambu-compatible path.
The Bambu-compatible path is used for Bambu Studio, FULU OrcaSlicer-bambulab, and OrcaSlicer when the call passes bambu_model:
- The machine preset always comes from
bambu_model(orBAMBU_MODEL, asked for when missing) andnozzle_diameter(defaultNOZZLE_DIAMETERor 0.4). The exact<model> <diameter> nozzlepreset must exist in the selected slicer installation. Itsinheritsandincludechains are resolved before the slicer runs. slicer_profile(orSLICER_PROFILE) is a process profile only. Amachine;processlist is rejected with instructions.- Slicing accepts
p1s,p1p,p2s,x1c,x1e,a1,a1mini,h2d,h2s, andh2cwhen the installed slicer has that preset. Printing still accepts only the seven models inBAMBU_MODEL. - The output must contain a nonempty
Metadata/plate_<n>.gcode. Failures stop with the slicer's exit code or signal, the tails of its output, and slicing-specific advice.
{
  "stl_path": "/path/to/phone-case.stl",
  "slicer_type": "bambustudio",
  "bambu_model": "p1s",
  "nozzle_diameter": "0.4",
  "bed_type": "textured_plate",
  "load_filaments": "/path/to/filaments/tpu-95a-hf.json",
  "arrange": true,
  "orient": false
}
Options for the Bambu-compatible path:
| Argument | What it does |
|---|---|
bed_type | Build plate: textured_plate, cool_plate, engineering_plate, or hot_plate (default BED_TYPE or textured_plate) |
nozzle_type | Installed nozzle: stainless_steel, hardened_steel, tungsten_carbide, or brass (default BAMBU_NOZZLE_TYPE, else the preset's stock nozzle). Printing requires it to match the printer's reported nozzle |
load_filaments | Filament profile JSON paths in slot order, ;-separated. One profile applies to every slot; otherwise give one per slot. PrusaSlicer and Slic3r take one .ini filament preset. filament_profile is an alias; get_printer_filaments reports a matching path as slots[].profile |
load_filament_ids | Comma-separated filament IDs mapping filaments to objects, such as 1,2,3,1 |
filament_colours | One #RRGGBB per filament slot, ;-separated. Defaults to the input 3MF's colours, then each profile's colour |
template_3mf_path, template_name, template_dir | Reuse a 3MF's or profile's slicer settings as the process profile (defaults: BAMBU_TEMPLATE_3MF_PATH, BAMBU_TEMPLATE_DIR). An explicit slicer_profile takes precedence |
uptodate, min_save, skip_modified_gcodes | Refresh 3MF presets to the installed slicer, write a smaller 3MF, or ignore custom G-code embedded in an input 3MF |
orient, arrange, ensure_on_bed, repetitions, clone_objects, skip_objects, slice_plate | Placement: auto-orient, auto-arrange (STL input is arranged by default; set false to keep a 3MF layout), drop floating models onto the bed, copies (OrcaSlicer copies an STL with --clone-objects), a total clone count for the loaded model, objects to skip, and which plate to slice (0 = all) |
scale, rotate, rotate_x, rotate_y | Transform before slicing (uniform scale; rotations in degrees). For OrcaSlicer STL input the server applies them to a mesh copy in Orca's order to avoid a CLI crash; see OrcaSlicer CLI limits |
enable_timelapse, allow_mix_temp | Insert timelapse parking moves; allow filaments with different temperature needs on one plate |
layer_height (mm), wall_loops (a whole number), and sparse_infill_density (such as "15%") are written over the selected profile on every slicer: as the process keys layer_height, wall_loops, and sparse_infill_density for Bambu Studio and OrcaSlicer, and as --layer-height, --perimeters, and --fill-density for PrusaSlicer and Slic3r. They win over a template. Cura refuses them; set them in its definition file. Your profile files are never modified.
Generic slicers keep their own profile formats: PrusaSlicer and Slic3r load one exported config, plus an optional filament preset .ini from load_filaments, and generic OrcaSlicer takes machine.json;process.json, optionally followed by |filament.json. slicer_type, slicer_profile, and filament_profile fall back to SLICER_TYPE, SLICER_PROFILE, and FILAMENT_PROFILE. The slicer executable comes from SLICER_PATH; a per-call slicer_path requires MCP_ALLOW_EXECUTABLE_ARG=1. See the slicing guide.
slice_with_template
Slice an STL or 3MF with a named template from the local template registry. The template supplies the process settings; the machine preset still comes from bambu_model and nozzle_diameter. It takes the same arguments as slice_stl, and an explicit slicer_profile in the call overrides the template.
{
  "stl_path": "/path/to/bracket.stl",
  "template_name": "p1s-petg-strong",
  "bambu_model": "p1s"
}
list_templates
List the saved slicing templates (.3mf, .json, .config) in the registry directory, BAMBU_TEMPLATE_DIR (default ~/Sync/bambu/templates), or in template_dir.
{}
save_template
Copy a local .3mf, .json, or .config file into the template registry. template_name defaults to the source filename without its extension.
{
  "source_path": "/path/to/p1s-petg-strong.3mf",
  "template_name": "p1s-petg-strong"
}
get_slice_settings
Read the slicer settings in a 3MF, an extracted project_settings.config, or a profile JSON without slicing: layer height, infill, walls, supports, brim, bed, printer, and filaments. Pass source_path, or template_name to read a saved template.
{
  "template_name": "p1s-petg-strong"
}
confirm_temperatures
Report every heater target in a G-code file: S and R forms, tool-addressed targets, RepRapFirmware G10/M568, and Klipper SET_HEATER_TEMPERATURE. An expected extruder_temp or bed_temp matches only when it equals the file's highest target, which the result returns as peak. It is read-only; the printing tools enforce their own safety gate.
{
  "gcode_path": "/path/to/model.gcode",
  "extruder_temp": 240,
  "bed_temp": 80
}
process_and_print_stl
Extend an STL's base, slice it, and print it through the same checked print gate as upload_gcode and print_3mf, including the human confirmation. If you pass extruder_temp or bed_temp, each must equal the sliced job's highest target (S and R forms, every tool); a mismatch stops before anything is uploaded. Pass material when the sliced G-code has no filament_type metadata. On a Bambu printer with a Bambu-compatible slicer, the sliced .3mf goes through the print_3mf checks, and the printer model is required.
{
  "stl_path": "/path/to/model.stl",
  "extension_inches": 0.1,
  "extruder_temp": 210,
  "bed_temp": 60,
  "material": "PLA",
  "type": "octoprint",
  "host": "192.168.1.100"
}
Use slice_stl, confirm_temperatures, and upload_gcode separately when you want to review the sliced file before the print is offered for confirmation.
Advanced Tools
Advanced Tools
Blender MCP
Connect a standard stdio Blender MCP server with BLENDER_MCP_COMMAND (for example, the full path to uvx) and BLENDER_MCP_ARGS (for example ["mcp-for-blender"]). The mcp-for-blender project was formerly published as blender-mcp, which still works as a compatibility wrapper. Install and enable its addon in Blender and start the addon's connection. Blender and this server must be able to read the same local files. Printer tools work without Blender configured. Keep Blender open while your agent works: the addon does not run in background mode. See the Blender guide for setup, units, and a worked example that refits a phone case for a new phone end to end.
blender_mcp_status
Inspect the Blender MCP configuration. With connect: true, it starts the configured server, initializes it, and lists its tools by name and summary. Pass tool_names to get the full input schemas of the tools you are about to call (include_schemas: true returns all of them, which is large). A successful connection does not prove the addon inside Blender is running; call get_scene_info through blender_mcp_call to check that.
{
  "connect": true,
  "tool_names": ["execute_blender_code"]
}
blender_mcp_call
Call a tool the Blender MCP server advertises, such as get_scene_info or execute_blender_code, with arguments matching its discovered schema. The full MCP result, including images and errors, is returned. Calls can change the active Blender scene and are never retried automatically. Preserve the user's own words in user_prompt when the remote tool asks for it.
{
  "tool_name": "get_scene_info",
  "arguments": { "user_prompt": "Inspect the scene before preparing a print." }
}
blender_mcp_export_stl
Export named objects from the live Blender scene to a new STL for slicing. Use it after modelling or editing through blender_mcp_call; Blender MCP's own export_scene writes GLB or FBX, not STL. The export writes world-space geometry with modifiers applied, without changing the scene, selection, or mode.
{
  "object_names": ["PhoneCase"],
  "output_path": "/path/to/phone-case.stl",
  "user_prompt": "Make it fit my iPhone 17 Pro Max."
}
- The result reports
output_verified: true, the triangle count, andbounding_box.dimensionsmeasured from the written file. Compare the dimensions with what you expect before slicing. - STL files carry no units and slicers read them as millimetres. An imported STL keeps its numbers, so the default
scale: 1is right. If a part was modelled in metres, the result warns that it is under 1 unit across; export again withscale: 1000. output_pathmust be new and its parent must exist; nothing is ever overwritten. On any Blender error, mismatched receipt, or invalid file, nothing is published.
blender_mcp_edit_model
Import an STL into Blender, apply ordered edits, and export a new STL. Supported operations are decimate:<ratio> (greater than 0, up to 1), remesh:<voxel size> (positive, in STL units), and boolean_union:<STL path>. Use blender_mcp_call for anything else.
{
  "stl_path": "/path/to/model.stl",
  "output_path": "/path/to/model-edited.stl",
  "operations": ["decimate:0.5"],
  "user_prompt": "Reduce the triangle count for printing.",
  "execute": false
}
- The default (
execute: false) validates the request and returns the plan and generated Python without launching Blender. Setexecute: trueto apply it, reusing the preview'soutput_path. - Omitting
output_pathselects a uniquemodel-edited-<id>.stlbeside the input. Existing input and output files are never overwritten. - The edit requires Object Mode, preserves existing scene objects and selection, and publishes the new STL only after checking a matching export receipt and a valid, finite triangle mesh. Binary STLs up to 256 MiB are validated in small chunks; ASCII STLs are limited to 4 MiB.
- Requests have connection, discovery, and call deadlines (
BLENDER_MCP_TIMEOUT_MS, default 120000) that also cover file validation. Interrupted edits are never replayed; inspect Blender before retrying, because an edit may already have started. - A valid STL is not proof of printability. Inspect the result before slicing.
Legacy BLENDER_MCP_BRIDGE_COMMAND shell commands remain supported when no standard command is configured. They receive JSON on stdin (modelPath, operations, source, and stlPath) and the same JSON in MCP_BLENDER_PAYLOAD, and their results report output_verified: false. A per-call bridge_command requires MCP_ALLOW_EXECUTABLE_ARG=1.
Fusion MCP
Design parts from scratch in Autodesk Fusion through faust-machines/fusion360-mcp-server, pinned to commit 19b9f1e95192. Set FUSION_MCP_COMMAND to the full path of uvx; FUSION_MCP_ARGS defaults to the pinned server in socket mode. Install that commit's Fusion360MCP add-in in Fusion and set it to Run on Startup. The client stays connected for the life of this server, only FUSION_* settings reach the Fusion server, and requests are never replayed. See the Fusion guide for setup, units, and the open-document requirement.
fusion_mcp_status
Report configured, connected, addinReachable, fusionRunning, the Fusion server's tools with their schemas, launched, pin (the faust-machines commit), and error when the server could not start. addinReachable means the add-in answered its own ping within 2 s on FUSION_MCP_PORT (default 9877, because Blender's MCP addon holds 9876). connected is true only when the add-in also answered through the Fusion server. With launch: true and Fusion not running on this Mac, it runs open -a "Autodesk Fusion" --env FUSION_MCP_PORT=<port> and waits up to 90 s for the add-in.
{ "launch": true }
fusion_mcp_call
Call any tool the Fusion server advertises, such as create_sketch, extrude, fillet, set_parameter, or execute_code, with arguments matching its discovered schema. The full MCP result and errors are returned, as for blender_mcp_call. Calls change the active design and are never retried. Fusion lengths are in centimetres unless a tool says otherwise.
{ "tool_name": "create_sketch", "arguments": { "plane": "xy" } }
fusion_mcp_new_design
Open a new parametric design document, so the Fusion tools have an active design. At the pinned commit, Fusion must already have some document open: no tool works from Fusion's home screen (issue #12).
fusion_mcp_export
Write <name>.stl (from export_stl), <name>.f3d (from export_f3d), and <name>.parameters.json (the design's user parameters) into output_dir, and return their absolute paths as stl, f3d, and parameters. The STL is one body: the only visible solid body, or body_name, whose name must be unique across all bodies, hidden ones and component copies included. It is checked as a finite triangle mesh, and stlUnits reports whether its numbers are millimetres. Existing files are never overwritten, and a failed export publishes nothing.
{ "output_dir": "/path/to/project", "name": "bracket" }
Available Resources
Available Resources
Resources follow the MCP resource protocol. They use the configured PRINTER_TYPE and credentials; the host segment selects the printer address.
printer://{host}/status: the printer's current status, as returned byget_printer_statusprinter://{host}/files: the file list, as returned bylist_printer_filesprinter://{host}/file/{filename}: details for one file. On Bambu printers this only reports whether the file exists.
For example, printer://192.168.1.100/status reads the status of the printer at that address.
Printer Limitations
Printer Limitations
- Status depth varies by backend.
get_printer_statusreturns each backend's own status data: Bambu includes progress, layers, and time remaining; OctoPrint's/api/printerand Moonraker's/printer/infohave no job progress. Usecounterpart_print_progressfor job progress on every backend. Its OctoPrint and Klipper mappings were checked against OctoPrint 1.8 and 1.11 virtual printers and a simulated Klipper printer; PrusaLink, Duet, Repetier, and Creality follow their API documentation and have not been checked on hardware. - Resume only what this server started.
resume_printrefuses a job it did not inspect and start, including one it started before a restart. Repetier's pause command and its time fields are not in Repetier's API manual. - Plain HTTP for most backends. OctoPrint, Klipper, Duet, Repetier, and Creality adapters connect over
http://. The Prusa adapter uses HTTPS for Prusa Connect, anhttps://host, or port 443. - Moonraker authentication is optional; Duet has no password support. Set
API_KEYfor Moonraker hosts that require authentication. Leave it empty only when Moonraker trusts the MCP host. A password-protected Duet cannot be reached yet. - Command sent is not print finished. A success response means the printer or its host accepted the request. Check status, and the printer itself, before you walk away.
- Bambu prints need a sliced project and the right model.
print_3mfneeds a.3mfwithMetadata/plate_<n>.gcode, uploads it tocache/, and starts plate 1. Print settings such as layer height and temperatures cannot be changed at print time.start_printhandles plain.gcodefiles only. - Bambu AMS mapping is simple.
ams_mappingvalues are sorted and padded to five entries; real behavior still depends on firmware, loaded filament, and the project's metadata. For AMS inventory and color matching, see bambu-printer-mcp. - Bambu temperatures go through G-code. Temperature targets are sent as
M104orM140over MQTT, so the printer's firmware and current state decide whether they apply. - Bambu networking assumes a trusted LAN. MQTT and FTPS use the printer's self-signed certificate. Uploads use TLS 1.2 with session reuse; confirmation on the X1C firmware reported in #22 is still outstanding.
- Safety checks read files and reports, not the physical printer. A declared material cannot prove what spool is loaded, which is why a human confirms. There is no bed check: the printer detects an occupied bed itself during bed leveling. Klipper macro parameters that name a heater are checked, but macro bodies stored on the printer cannot be inspected. On Duet/RepRapFirmware, selecting a tool (
T0) heats it to the temperature already stored on the printer; activation-onlyM568andM144are refused, but a plain tool change is allowed because every firmware uses it. The safety gate is tested with mocked printer transports and loopback HTTP APIs, plus one real Bambu P1S run that reached the firmware's command check; other printer systems have not been exercised on real hardware in this release. - Remote starts need a download route.
start_printof a file already on the printer works on Bambu Lab, OctoPrint, Klipper, and Duet. Repetier, Prusa, and Creality refuse it; upload the local G-code withprint: trueinstead.
General Limitations and Considerations
General Limitations and Considerations
Memory usage
- STL tools load the whole mesh into memory as Three.js geometry. Files over about 10 MB can use several hundred MB of RAM.
- Running several operations in a row on large files can build up memory between garbage collection cycles.
- There is no built-in memory cap. On constrained systems, avoid processing several large files at once.
STL manipulation limitations
lay_flatlooks for the largest flat face; results on organic or rounded models can be unpredictable.extend_stl_baseadds new geometry beneath the model. Complex or non-planar undersides can produce gaps or intersections at the join, so inspect the result.merge_verticeswith a large tolerance can change the model's shape. The 0.01 mm default is safe for most models.modify_stl_sectionworks best on simple geometry. Non-manifold meshes (holes, overlapping faces, internal geometry) can produce unexpected results for any transformation; repair them first in your slicer or a mesh tool.
Visualization limitations
generate_stl_visualizationproduces a simplified schematic, not a true 3D render, and very detailed models may lose detail.
Performance considerations
- Slicing can take from seconds to several minutes, depending on the model and your CPU. Slicer runs time out after
SLICER_TIMEOUT_MS(10 minutes by default). - Large uploads depend on your network and the printer's storage speed.
- Bambu MQTT connections are reused. If a printer restarts or the network drops, the next call reconnects.
MCP Safety Notes
MCP Safety Notes
Prompt injection is an open problem for tool-using agents. A downloaded model's description, a README inside an archive, 3MF metadata, or a web page can all contain instructions aimed at your agent. Practical mitigations:
- Treat tool output and downloaded files as untrusted input.
- Keep printer keys and access codes in server configuration, with the least privilege your printer software allows.
- Keep per-call executable selectors off. Slicer, bridge, and Blender commands come from server configuration unless
MCP_ALLOW_EXECUTABLE_ARG=1is set. - Keep print confirmation on. The server asks a human through MCP elicitation before every print start and positive heating command, and refuses clients that cannot ask.
PRINT_REQUIRE_CONFIRMATION=0(all printers) orBAMBU_REQUIRE_CONFIRMATION=0(Bambu only) opts out for headless setups; the first print after a finished job still asks. - Heater ceilings come only from server configuration (
PRINTER_MAX_NOZZLE_TEMP,PRINTER_MAX_BED_TEMP,PRINTER_MAX_CHAMBER_TEMP, or Bambu's per-model limits). Tool arguments and G-code never raise them. - Run the streamable HTTP transport on a trusted network. It binds to
127.0.0.1by default and has no built-in authentication. - Set
BAMBU_MODELcorrectly and never substitute a similar model.


